Pharmaceutical cartoning brings the primary pack, carton and any required leaflet together into the finished presentation. A useful process specification follows each component through insertion, identification, closure and inspection, including the route taken by a rejected pack.
Define the checks at each step
| Step | What to establish | Example acceptance check |
|---|---|---|
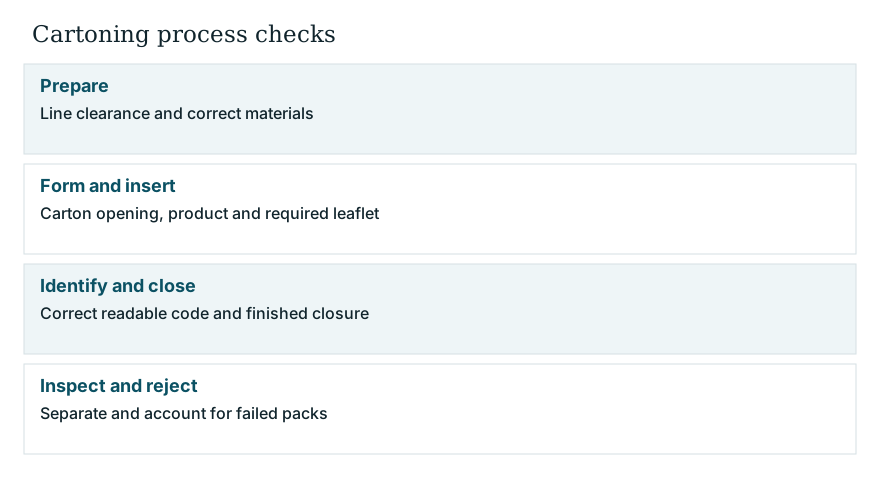
| Line clearance | Correct materials and removal of the previous job | Documented pre-start inspection |
| Carton supply and forming | Correct blank, orientation and usable opening | Formed carton matches the approved drawing |
| Product insertion | Correct presentation and quantity | Required contents are present |
| Leaflet insertion | Correct version and presence where required | Missing or incorrect leaflet is detected |
| Coding and closure | Correct readable code and closed carton | Check code content and closure condition |
| Reject handling | Failed packs are separated and accounted for | Challenge the reject device and reconcile test packs |
US 21 CFR 211.130 requires procedures for correct packaging and labeling, pre-use checks and documented line clearance. The equipment configuration should support those procedures, including a clear response when a component or identification check fails.
Challenge the failure response
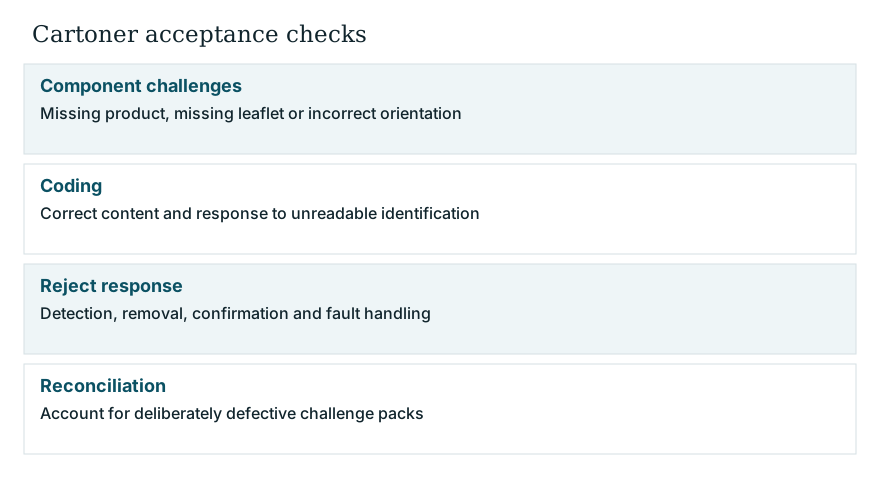
A sensor signal alone does not establish that the pack reached the reject container. Include the detection, reject action and response to a reject fault in the acceptance plan. The test conditions should make clear which deliberately defective test packs are introduced, how they are tracked and how they are removed from production.
Check the response to missing components, incorrect orientation or unreadable coding where those functions are part of the specified system. The responsible quality and engineering teams should approve the challenge method and acceptance criteria before the test.
Compare output under the same conditions
Express the required output in good cartons per minute for a stated pack configuration. Include carton dimensions, primary-pack quantity, leaflet format and coding requirements. Record changeover and stoppage time separately from the operating rate so that a proposal can be compared with the production schedule.
EU GMP Annex 15 treats the user requirements specification as a reference through the validation lifecycle. Carry the agreed cartoning checks into that document and trace them to the applicable design review and qualification activities.
Use packaging-line selection for an output calculation, horizontal vs vertical cartoning machine to match side-load, vertical end-load or top-load orientation to container stability and leaflet path, cartoning machine leaflet and tuck checks for inline folder, pharmacode and closure sensors, and the URS checklist for requirement fields. The overwrapping guide covers the next operation when film is applied around the carton.